Leading Belt Conveyor Manufacturer in India for Efficient Material Handling
Efficient material transportation is essential for improving productivity, reducing manual labor, and ensuring smooth industrial operations. Shree Techno Engineers is a trusted Belt Conveyor Manufacturer, Supplier, and Exporter in India, offering high-performance and customized conveyor systems for a wide range of industries.
Established in 2002, we specialize in designing and manufacturing robust Industrial Belt Conveyors that provide reliable, continuous, and cost-effective transportation of bulk materials. Our conveyor systems are engineered for maximum efficiency, low maintenance, and long service life, making them ideal for industries such as power plants, cement plants, mining, steel, chemical, fertilizer, food processing, and other process industries.
Whether you require a Flat Belt Conveyor, Inclined Belt Conveyor, Troughed Belt Conveyor, or a customized Material Handling Conveyor System, our experienced engineering team delivers solutions tailored to your operational requirements. Explore our complete range of Material Handling Equipment on our Home Page.
What is a Belt Conveyor?
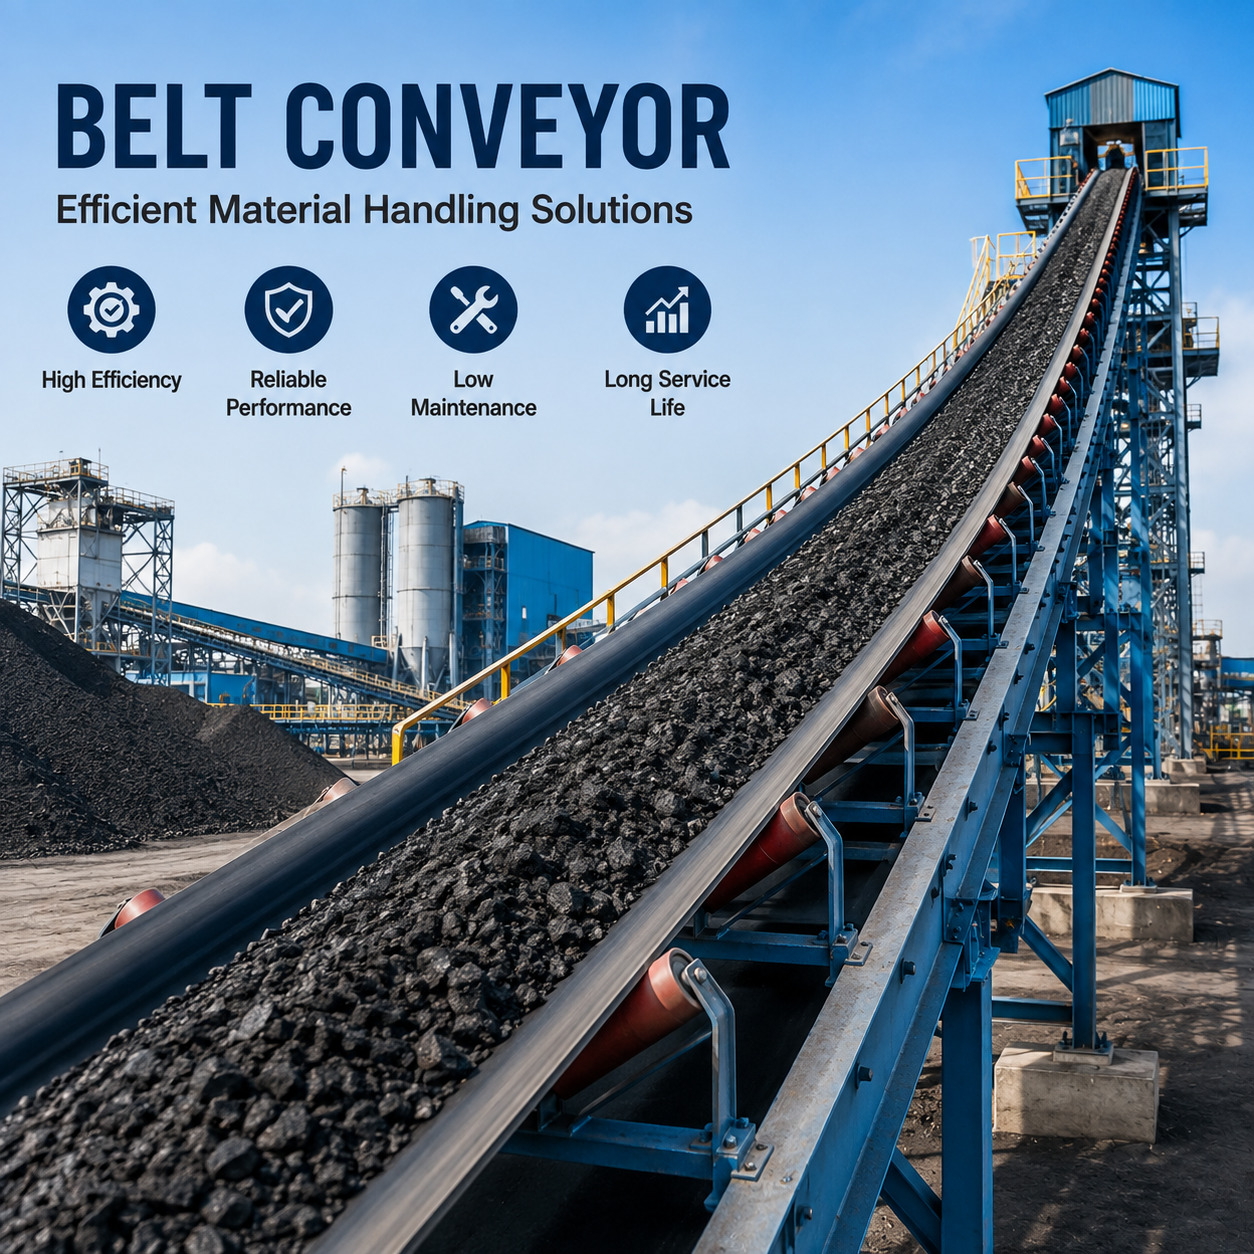
A Belt Conveyor is one of the most widely used Material Handling Equipment designed to transport bulk materials and finished products efficiently over short and long distances. It consists of a continuous belt moving over rollers or pulleys, allowing smooth, safe, and uninterrupted material movement.
Belt conveyors reduce manual handling, improve productivity, minimize product damage, and optimize production processes across various industries.
How Does a Belt Conveyor Work?
A belt conveyor operates by using an electric motor to drive a pulley, which moves the conveyor belt continuously. Materials are placed on the moving belt and transported from one location to another with minimal effort and maximum efficiency.
Depending on plant requirements, the conveyor system can be integrated with Coal Crushers, Bucket Elevators, Screw Conveyors, Ash Handling Systems, Pneumatic Conveying Systems, and Rotary Airlock Valves to create a complete material handling solution.
Types of Belt Conveyors
We manufacture various types of belt conveyors to meet different industrial applications.
Each conveyor is designed according to material characteristics, conveying distance, load capacity, and plant layout.
Key Features
Benefits of Our Belt Conveyors
Installing a high-quality belt conveyor offers several operational advantages.
Continuous Material Handling
Reduced Operating Costs
High Efficiency
Flexible Design
Safe Operation
Low Maintenance
Reliable industrial equipment is built on proven quality management systems and precision engineering. Manufacturers following internationally recognized standards ensure consistent product quality and reliability. Learn more about the ISO 9001 Quality Management System.
Applications
Our Industrial Belt Conveyors are widely used in:
Industrial material handling systems should also comply with environmental and dust control regulations wherever applicable. For additional environmental guidelines, visit the Central Pollution Control Board (CPCB).
Technical Specifications
We manufacture belt conveyors in various configurations based on customer requirements.
Related Material Handling Equipment
To provide complete industrial solutions, we also manufacture:
Why Choose Shree Techno Engineers?
Since 2002, Shree Techno Engineers has been delivering reliable Material Handling Equipment to industries across India and international markets.
Why Customers Choose Us
Frequently Asked Questions
Partner with Shree Techno Engineers
Looking for a reliable Belt Conveyor Manufacturer in India?
Shree Techno Engineers offers durable, high-performance, and customized Industrial Belt Conveyors designed to maximize productivity, improve operational efficiency, and reduce maintenance costs. Contact our engineering team today to discuss your project requirements through our Contact Us page.